3D Print your own HK G3/CETME Magazine Release and Stock Pin Bushing Drilling Jig
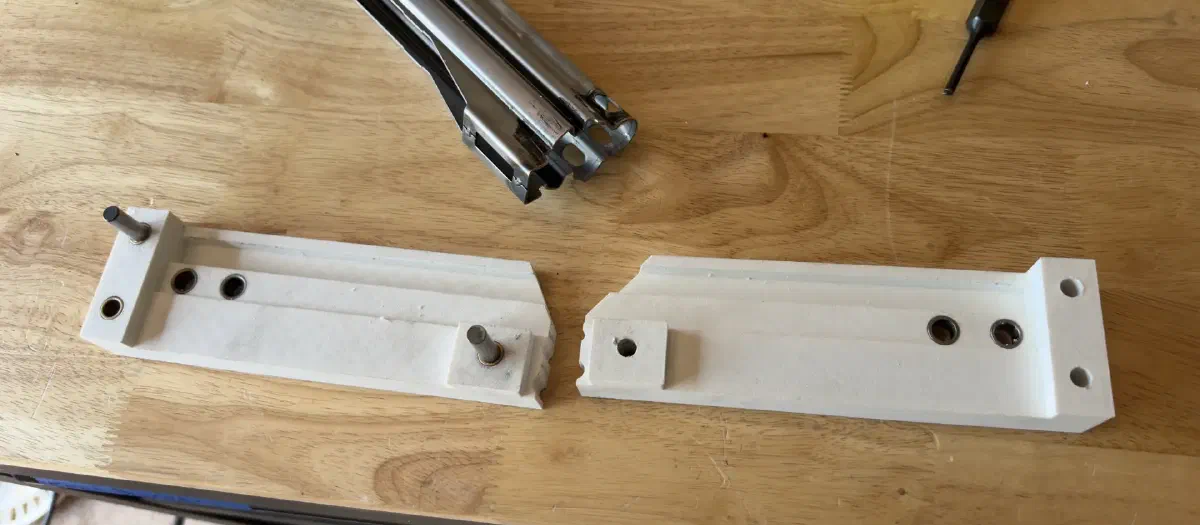
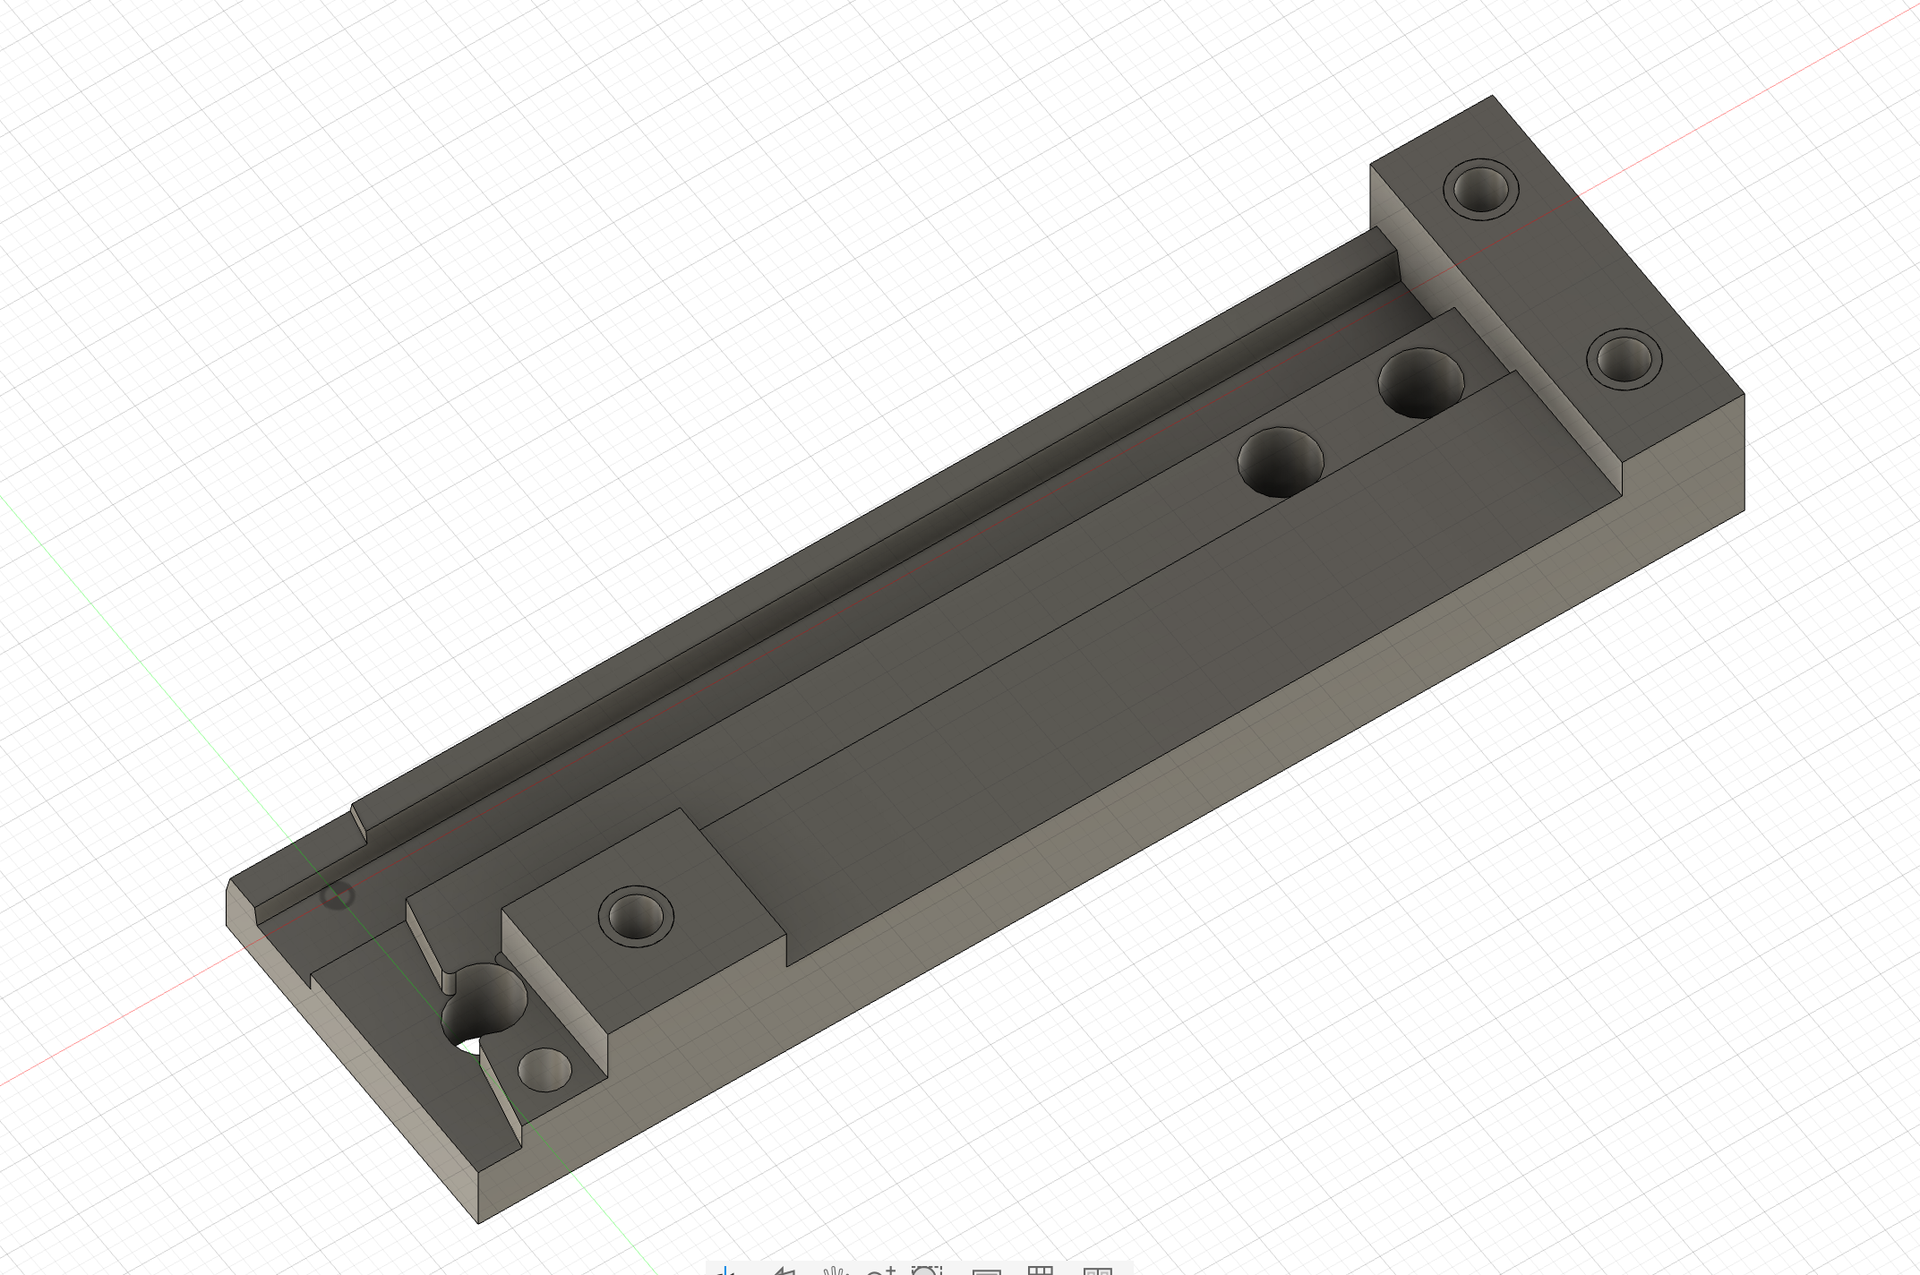
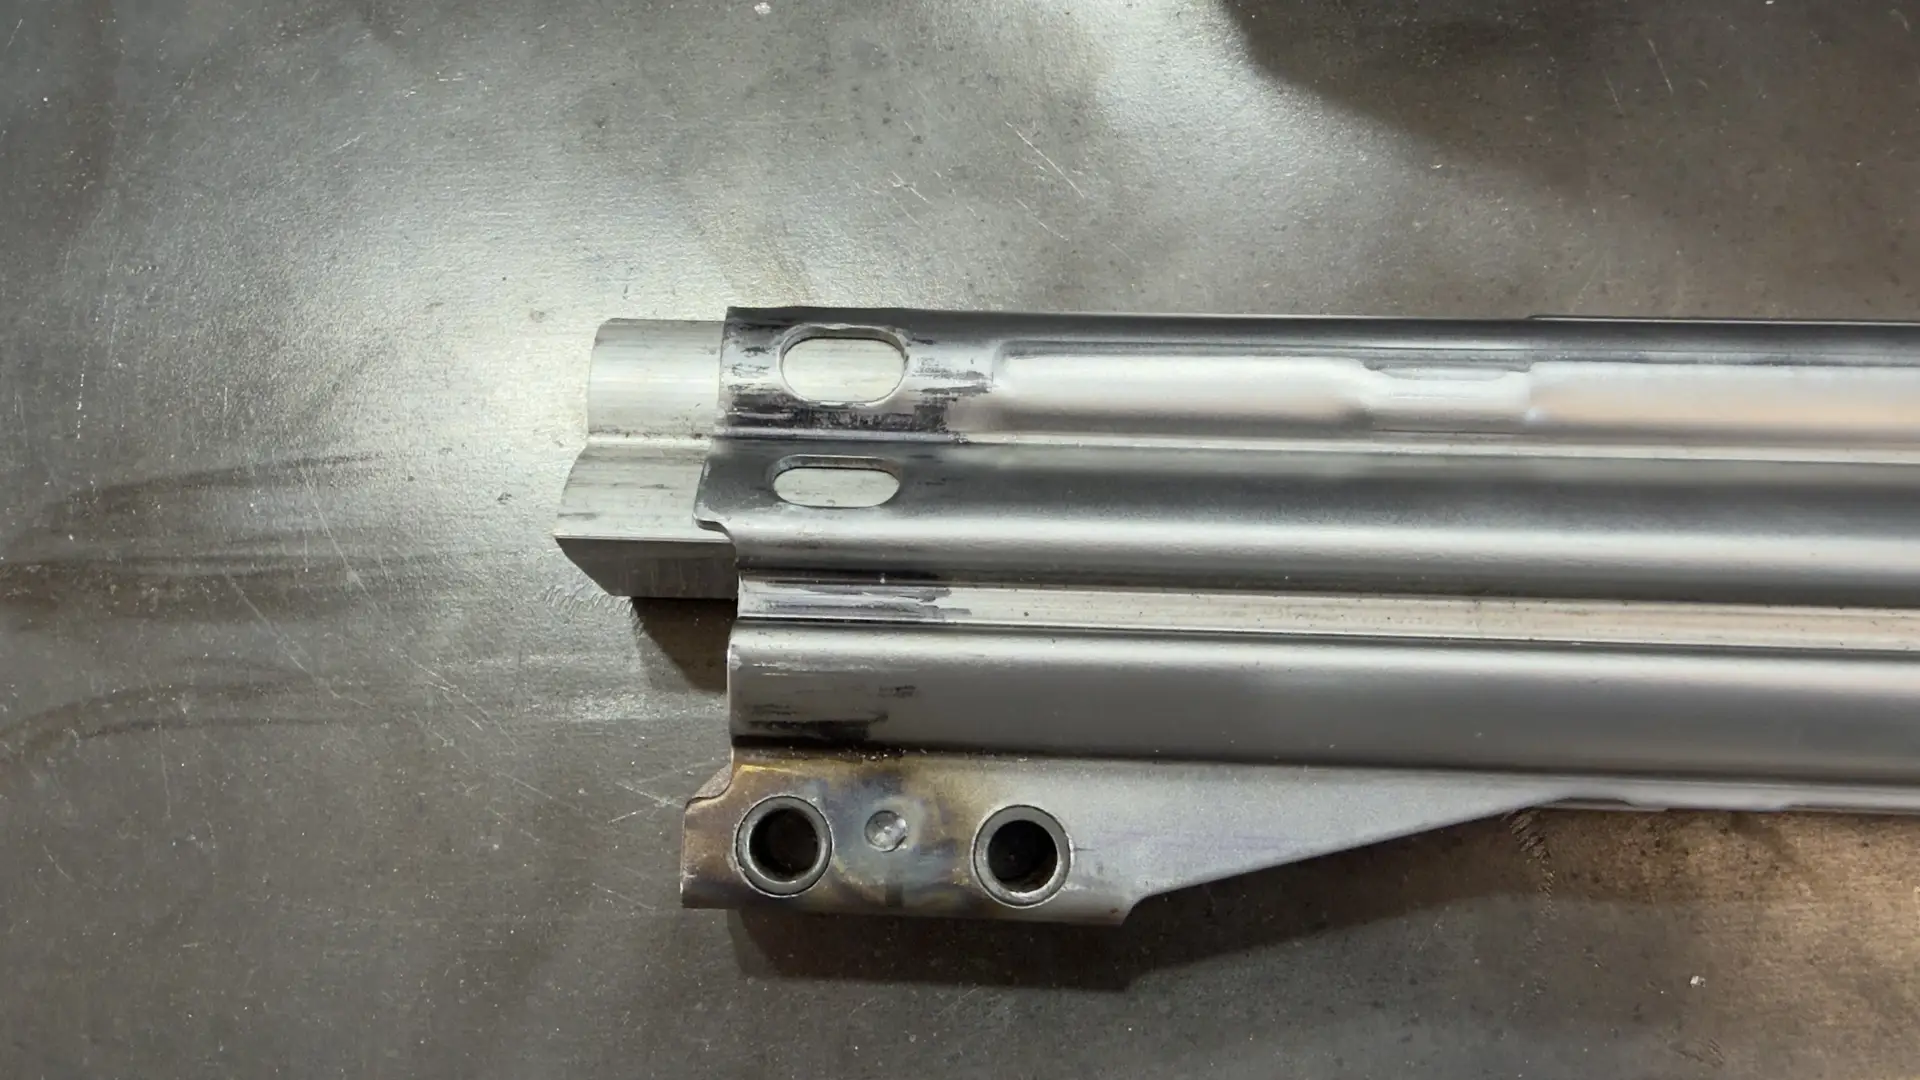
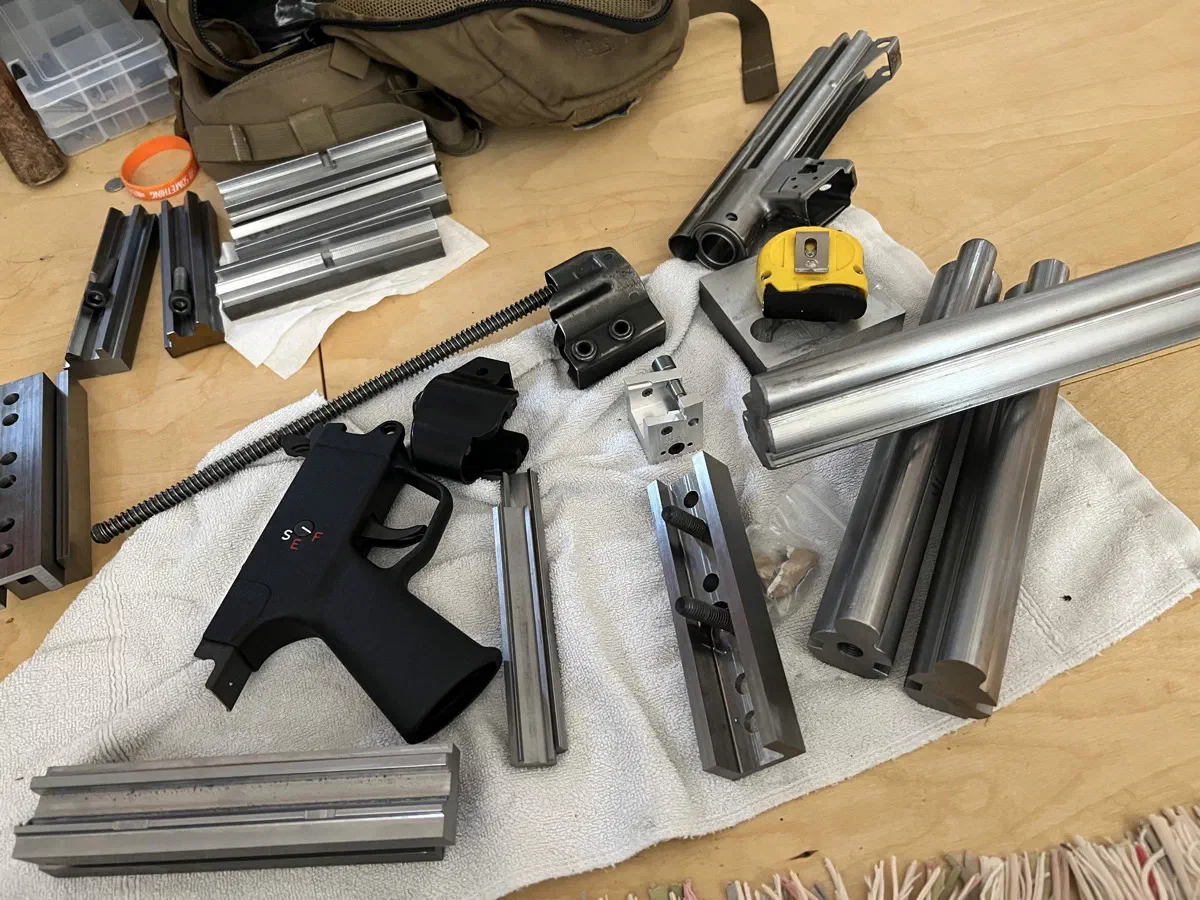
This drilling jig, when paired with the below drill bushings and pins, can be used to accurately place the stock pin bushing, mag release, and paddle mag axle holes. It can also serve as a reference file to take dimensions from this part of the HK G3/MP5 receiver. Dimensions are taken from 3D scans and verified against the MP5 blueprints–my scans were within .01mm of the specified values on the print. Unlike other jigs, this jig accurately locates all holes based on the datums specified in the original prints: the dead center of the receiver rails, and the rear of the magwell stamping.
Download all Fusion files associated with this article here: https://marbleduck.com/resources/g3-drill-jig.f3d
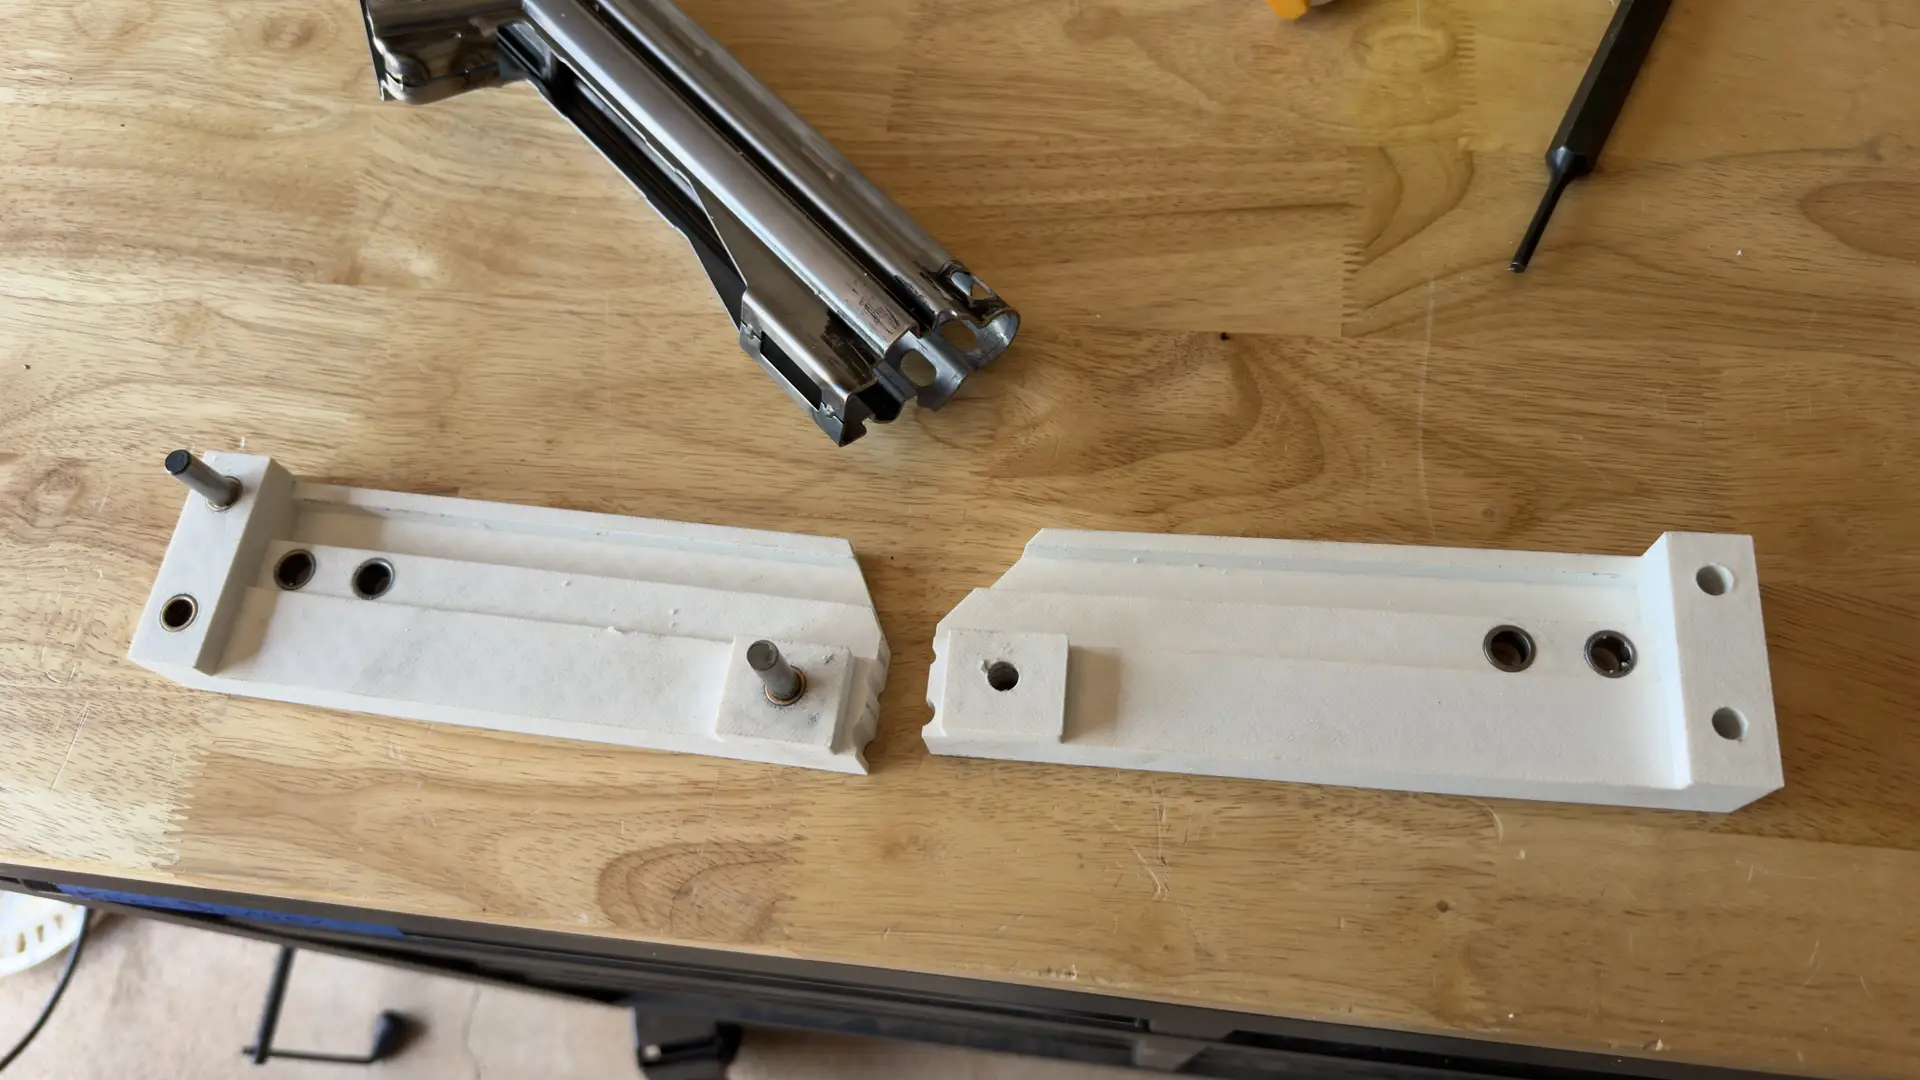
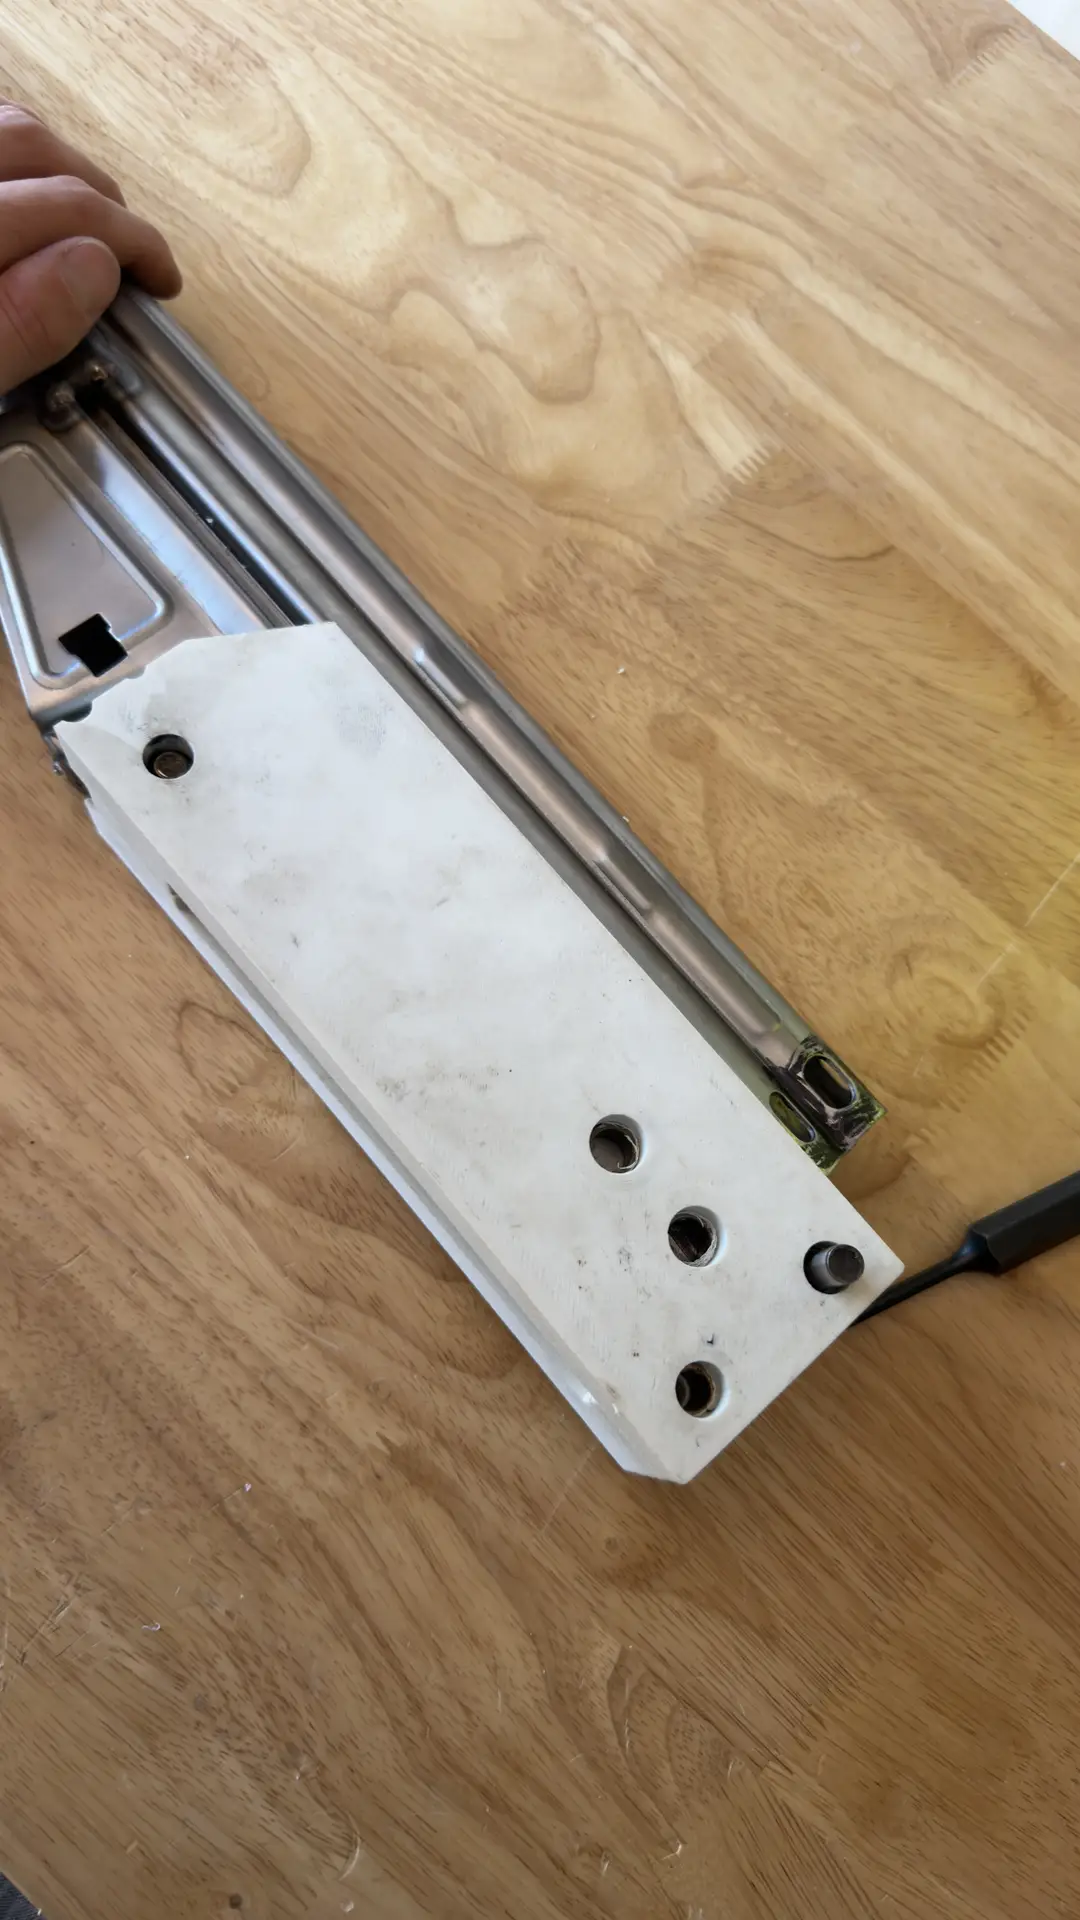
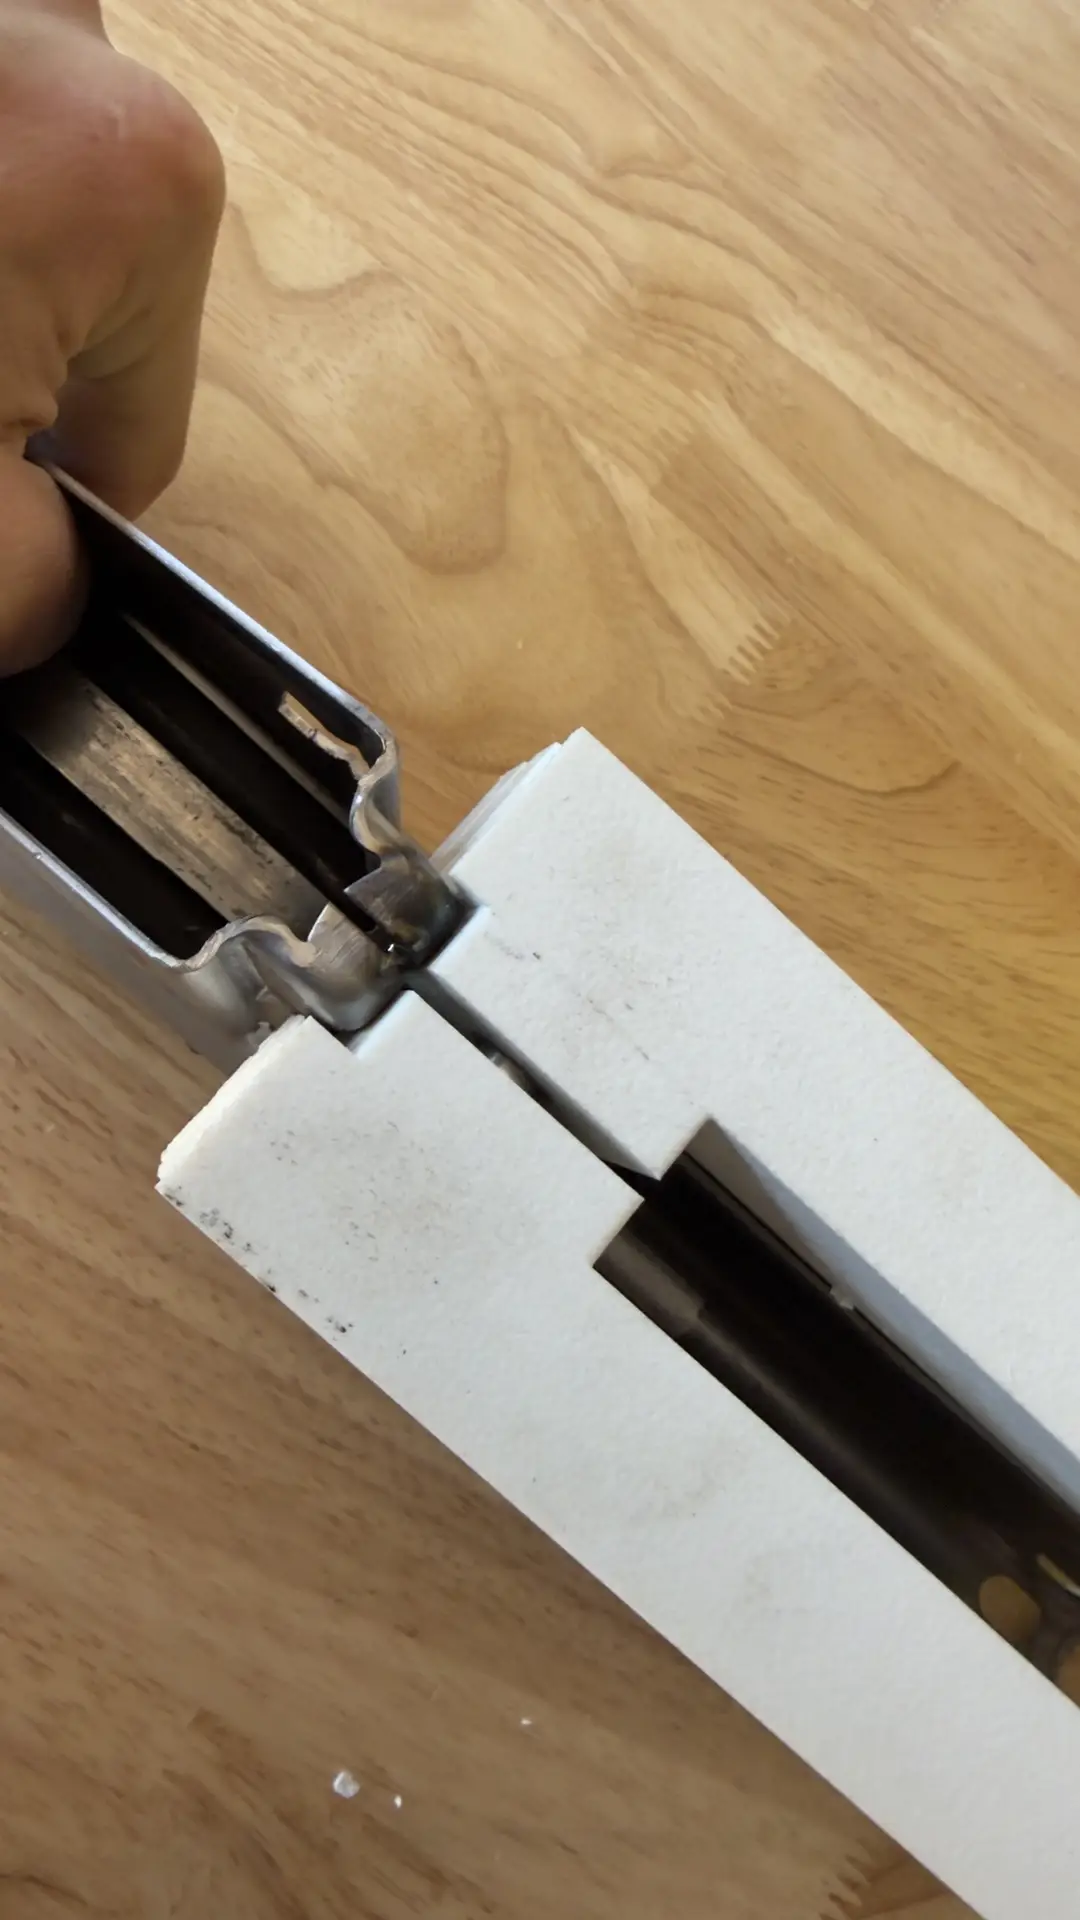
USAGE: Once assembled with the correct bushings and locator pins, place the correspondingly-shaped rails into the rail indents on the outside of the HK receiver. Index the back of the magazine well against the square boss, as shown in the last picture. Clamp together, ensuring jig remains flat and parallel. Place in drilling machine of your choice. Drill. Thanks to the design of this jig, I am easily able to maintain the HK specified tolerance of <.01mm deviation for each of these holes relative to one another even when using a rickety drill press.
LOCATOR PINS: Using the vertical pin bosses and some 5/16" pins, you can accurately locate both halves of the jig together. 5/16" pins can be pressed into one half of the jig, and the other half of the jig can take the linear bearings (6391K165).
REAR STOCK PIN HOLES: Press the .375 ID bushings (8491A726) into all four of these holes. Ensure they are flush with the side contacting the receiver. This is adequate for the .372 OD HKParts bushings, but 10mm original HK-build bushings should use a 10mm bushing and drill. It is acceptable to drill at .375 with the jig and ream to 10mm for this application.
Need .375 OD bushings? Don’t pay $5 a pop plus shipping from HKParts. Get 3 feet of 89955K159 3/8 Chromoly Tube from Mcmaster, which happens to be the perfect ID with a 3/8 OD. I’m pretty sure this is what HKParts cuts up to make their bushings.
PADDLE MAG AXLE PIN: Currently set up for a 3/16" axle pin since those are the ones I use/make. Typically these are 1/8", but a 3/16 axle pin lets you cut up and ream out an original bushing and front push pin to use instead of buying the HKparts ones. Comply with all federal regulation.
MAG RELEASE PIN: There are different sized bushings for L and R halves. Use the correct one. Press them in only deep enough to not run into the magwell geometry.
PARTS LIST Optionally included are the odd-sized drills and reamers you might need. If you already have these or intend to use different sizes, they do not need to be purchased. Given with McMaster-Carr part number to make it easier to find the correct item.
- 2 Each 2901A144 Black-Oxide High-Speed Steel Drill Bit Jobbers’, B Bit Size
- 2 Each 28255A53 Black-Oxide High-Speed Steel Short-Length Drill Bit 8 mm Bit Size
- 1 Each 3671N149 Press-Fit Drill Bushing 0.315" ID, 1/2" OD, 1/2" Long
- 1 Each 96511A874 Press-Fit Drill Bushing 0.238" ID, 13/32" OD, 3/8" Long
- 1 Each 8803A601 High-Speed Steel Round-Shank Reamer with Straight Flute, 0.3130" Reamer
- 3 Each 6391K165 Oil-Embedded 841 Bronze Sleeve Bearing for 5/16" Shaft Diameter and 7/16" Housing ID, 3/4" Long
- 2 Each 8491A107 Press-Fit Drill Bushing 0.1875" ID, 5/16" OD, 1/2" Long
- 4 Each 8491A726 Press-Fit Drill Bushing 0.375" ID, 1/2" OD, 3/8" Long
- 1 Pack of 10 each 98381A591 Dowel Pin Alloy Steel, 5/16" Diameter, 2" Long